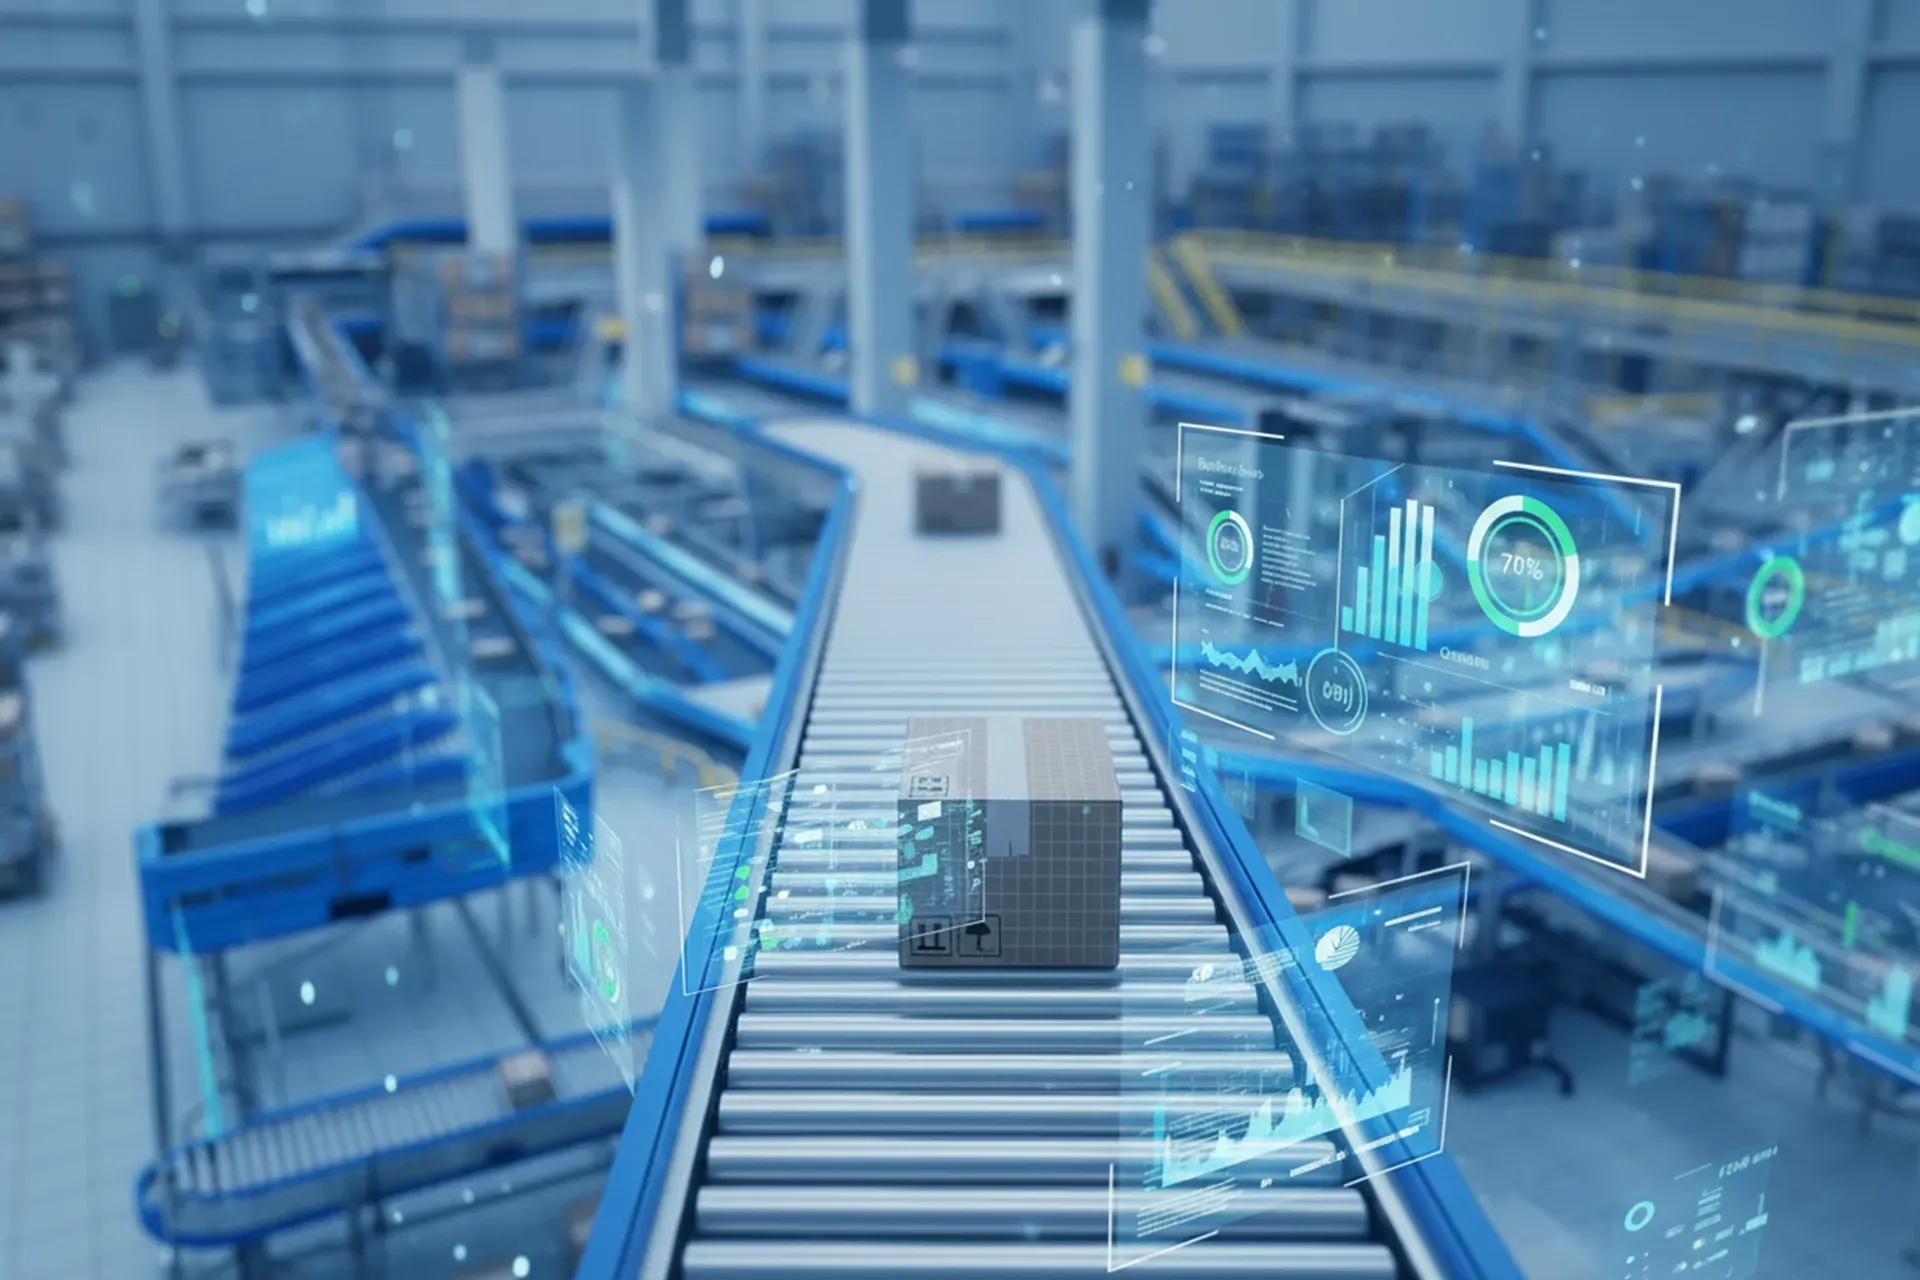
Warehouse automation simulation helps optimize conveyor throughput by creating a virtual replica of your conveyor system, allowing engineers to identify bottlenecks, test layout changes, and validate capacity before a single physical component is moved or installed. It gives operations teams a risk-free environment to run hundreds of scenarios and find the configuration that delivers the highest throughput. The questions below unpack exactly how this works in practice.
What bottlenecks most commonly limit conveyor throughput in automated warehouses?
The most common bottlenecks that limit conveyor throughput in automated warehouses are merge points, sortation junctions, induction stations, and scanner or divert gates where product accumulates faster than it can be processed. These pinch points are often invisible until the system runs at peak volume, which is precisely why they are so difficult to catch during manual planning.
In practice, throughput loss rarely comes from a single catastrophic failure. It builds up from a combination of smaller inefficiencies that compound under load. The most frequently observed culprits include:
- Merge conflicts at conveyor junctions where two product streams compete for the same lane
- Induction pacing mismatches where operators feed product faster or slower than the downstream sorter can handle
- Accumulation zone sizing that is too short to buffer demand spikes, causing upstream stoppages
- Scan-no-read events at barcode readers that divert products to exception handling and disrupt flow
- Maintenance-related downtime on high-frequency components like transfers and pop-up wheels that creates ripple effects across the line
What makes these bottlenecks tricky is that they shift depending on order profile, product mix, and time of day. A merge point that performs fine during standard operations may become a hard constraint during peak season when order volume doubles. This dynamic nature is exactly why static analysis tools like spreadsheets consistently underestimate the problem.
How does discrete-event simulation model conveyor system behavior?
Discrete-event simulation models conveyor system behavior by representing every physical component, product unit, and operational event as a dynamic object that interacts in real time. The simulation advances through time step by step, processing events such as a tote arriving at a merge point or a sorter completing a divert cycle, and calculating the downstream effects of each event on the rest of the system.
In a discrete-event model, each conveyor segment, scanner, divert gate, and workstation is built from a component with defined rules: speed, capacity, cycle time, failure rate, and logic for how it handles product under different conditions. Products move through this virtual network just as they would in a real warehouse, accumulating, merging, sorting, and queuing according to the rules you define.
This approach captures behavior that aggregate calculations simply cannot, including the interaction effects between components. For example, a DES simulation model can show how a 0.3-second delay at a label applicator creates a queue that backs up into an induction zone 40 meters away during a burst of high-velocity SKUs. That kind of cause-and-effect chain is invisible in a spreadsheet but immediately visible in a discrete-event simulation running in real time or accelerated time.
Our Enterprise Dynamics simulation platform uses a drag-and-drop atom-based approach, where pre-built components representing conveyors, sorters, buffers, and workstations are assembled into a full virtual model of your warehouse system. As a purpose-built DES simulation platform for warehousing and intralogistics, it can be connected to real WMS and ERP data, making the simulation a true digital twin of your operation rather than a theoretical approximation.
Build your own simulation, your way
Enterprise Dynamics gives developers full control to model, scale, and integrate complex systems with C++, APIs, and real-time data.
Explore Enterprise DynamicsWhat types of what-if scenarios can simulation run on a conveyor layout?
Simulation can run virtually any what-if scenario that changes the physical layout, operational rules, or demand conditions of a conveyor system. This includes testing additional sorter lanes, adjusting induction rates, rerouting product flows, simulating equipment failures, and modeling peak-season volume surges, all without touching the live system.
The most valuable scenario categories for conveyor optimization fall into three areas:
- Capacity and throughput scenarios: What happens to throughput if induction rate increases by 20%? Can the current sorter handle projected volume in three years? What is the maximum sustainable cartons-per-hour before the system degrades?
- Layout and routing scenarios: Would adding a second merge lane at junction B eliminate the bottleneck? Is it more efficient to route returns through the main sorter or a dedicated loop? What is the impact of relocating a workstation 15 metres upstream?
- Resilience and failure scenarios: How does throughput recover if a key divert gate goes offline for 20 minutes? What is the downstream effect of a scanner outage at the main induction point? Does the accumulation buffer have enough capacity to absorb a 10-minute upstream stoppage?
Being able to run these scenarios before committing to capital expenditure is one of the most direct ways simulation delivers ROI. A layout change that looks logical on a CAD drawing may create an unexpected bottleneck in simulation, saving significant rework costs.
How accurate is warehouse simulation for predicting real conveyor performance?
Warehouse simulation software is highly accurate for predicting real conveyor performance when the model is built with reliable input data and validated against actual system measurements. A well-calibrated simulation typically predicts throughput, cycle times, and queue behavior within a margin that is close enough to real-world results to support confident investment decisions.
Accuracy depends on three factors above all others. First, the quality of input data: conveyor speeds, cycle times, failure rates, and product dimensions need to reflect reality, not design specifications. Second, the fidelity of the model logic: rules governing merges, divert decisions, and accumulation behavior must match how the real control system operates. Third, validation: the model should be tested against known historical performance data before it is used for forward-looking analysis.
Where simulation is most reliable is in predicting relative performance differences between scenarios. Even if the absolute throughput number is slightly off, the simulation consistently identifies which configuration outperforms another and by how much. This comparative accuracy is what makes it so useful for decision-making, because the goal is rarely to predict one exact number but to determine which option is better and why.
When should a warehouse run a conveyor simulation, before or after installation?
A warehouse should run conveyor simulation before installation, ideally during the design and procurement phase. Running simulation before physical installation allows teams to catch layout flaws, validate capacity assumptions, and test control logic while changes are still inexpensive. Post-installation simulation still adds value, but the cost of acting on its findings is significantly higher.
The timeline for simulation in a conveyor project typically looks like this: early design validation comes first, where the simulation confirms that the proposed layout can meet throughput targets under normal and peak conditions. This is followed by scenario testing during detailed engineering, where specific design decisions, such as sorter model selection or accumulation zone lengths, are stress-tested. Finally, pre-go-live testing uses the simulation to train operators and validate control logic before the system goes live.
Post-installation simulation is not without value. Warehouses that are already operational use intralogistics simulation to diagnose persistent throughput problems, evaluate expansion options, and prepare for seasonal peaks. But the leverage is greatest before concrete is poured and equipment is bolted down. Changes that cost very little in a model can cost a great deal once a conveyor system is installed and running.
How Enterprise Dynamics helps optimize conveyor throughput
Enterprise Dynamics is our discrete-event simulation software platform built specifically for the kind of complex, high-speed conveyor and intralogistics environments described throughout this article. It gives engineers and operations teams the tools to model, test, and optimize conveyor systems before and after installation, with a level of detail that spreadsheets and static tools cannot match.
Here is what Enterprise Dynamics brings to conveyor throughput optimization specifically:
- Pre-built conveyor and sortation components that can be assembled into a full virtual warehouse model using a drag-and-drop interface
- Real-time 2D and 3D visualization so teams can see exactly where congestion builds and how product flows through the system
- WMS and ERP integration to run simulations on real order data rather than theoretical demand profiles
- What-if scenario testing across layout changes, induction rates, equipment failures, and peak volume conditions
- Bottleneck identification and KPI reporting that quantifies throughput loss and supports the business case for investment decisions
Whether you are designing a new automated warehouse, expanding an existing facility, or troubleshooting a throughput problem that keeps surfacing at peak, Enterprise Dynamics gives your team the insight to act with confidence. As a leading DES simulation tool for warehousing and material flow optimization, it is designed to support decisions at every stage of a project. Get in touch with us to discuss how simulation can be applied to your conveyor system.
Frequently Asked Questions
How long does it typically take to build a conveyor simulation model for a warehouse?
The time required depends on the complexity of the conveyor system, but most mid-sized warehouse simulation models can be built in two to six weeks when good input data is available. Platforms like Enterprise Dynamics accelerate this significantly through pre-built conveyor, sorter, and buffer components that don’t need to be coded from scratch. The longest part of the process is usually data collection and validation, not model construction itself, so having accurate conveyor specs, cycle times, and historical throughput data ready before the project starts makes a measurable difference.
What data do I need to provide before running a conveyor simulation?
At a minimum, you need conveyor segment speeds, product dimensions and weights, sorter cycle times, induction rates, scanner read rates, equipment failure frequencies, and a representative order or demand profile. Real operational data is always preferable to design specifications, since as-built systems often behave differently from what was originally planned. If you’re simulating a new installation, supplier-provided specs are a reasonable starting point, but the model should be revisited and recalibrated once the system goes live and real performance data becomes available.
Can simulation help if our conveyor system is already installed and we're experiencing throughput problems?
Yes, post-installation simulation is a well-established approach for diagnosing persistent throughput issues that are difficult to isolate in a live environment. By building a digital twin of your existing system and feeding it real order data, engineers can reproduce the problem conditions in the model, test potential fixes, and validate a solution before making any physical changes. This is particularly valuable when the root cause isn’t obvious, since simulation can reveal upstream or downstream interaction effects that aren’t visible from observing a single point on the line.
What's the difference between using simulation and just running a pilot test on the physical system?
Physical pilot tests can only test one configuration at a time, carry the risk of disrupting live operations, and are expensive to repeat if the results are inconclusive. Simulation allows you to run hundreds of configurations in parallel, at any time of day, with no risk to throughput or service levels. The two approaches are most powerful when used together: simulation narrows the field to the best one or two options, and a targeted physical test then confirms the winner under real conditions, reducing both risk and the number of costly live trials needed.
How do we know when a simulation model is accurate enough to trust for major investment decisions?
A simulation model is considered investment-ready when it has been validated against at least one set of known historical performance data and produces results within an acceptable margin of real-world measurements. The standard validation approach is to replay a past operational period through the model and compare simulated throughput, queue lengths, and cycle times against what was actually recorded. Even if absolute numbers show a small variance, the model is reliable for decision-making when it consistently ranks configurations in the same order as real-world tests would, which is the comparative accuracy that matters most for capital decisions.
Can simulation model the impact of staffing levels and operator behavior on conveyor throughput?
Yes, staffing and operator variability can be incorporated into a simulation model as controllable parameters. Induction operator pacing, pick station dwell times, exception handling speeds, and shift changeover gaps can all be modeled with realistic variability ranges rather than fixed values, making the simulation reflect actual human performance rather than ideal conditions. This is especially useful for identifying whether a throughput problem is equipment-driven or process-driven, since the two require very different solutions.
What's a common mistake teams make when using simulation to optimize conveyor throughput for the first time?
The most common mistake is over-optimizing for a single scenario, typically average daily volume, without stress-testing the model against peak conditions and edge cases. A conveyor layout that looks efficient at average throughput can degrade significantly when order volume spikes, product mix shifts, or a single component goes offline. Best practice is to define a range of test scenarios upfront, including at least one failure scenario and one peak-volume scenario, before drawing any conclusions from the simulation results.
Related Articles
- What is the benefit of real-time data integration in digital twin warehouse software?
- What is the difference between warehouse simulation software and ERP planning tools?
- How is supply chain simulation software used in port operations?
- What are the best alternatives to AutoMod simulation software?
- What is scenario analysis in supply chain simulation software?